Hydroxyl Resin Hardener Cures That Stay Soft, Explained
Hydroxyl Resin Hardener Cures Can Stay Soft for Several Fixable Reasons
A Hydroxyl Resin Hardener is a crosslinking chemical additive used to convert liquid hydroxyl-functional resins into a hardened, chemically stable film. In practical terms, it reacts with the -OH groups in a resin system to build a network structure that resists solvents, abrasion, and moisture once fully cured. When quality engineers see a film that stays soft, tacky, or "green" long after the specified cure window, the hardener itself is often blamed first — but the real cause frequently sits somewhere in the ratio, the mixing process, or the cure environment. This article walks through what the product actually does, what types exist, and how to work backward from a soft film to the exact failure point.
Types of Hydroxyl Resin Hardener Systems
Not every hardener behaves the same way, and picking the wrong type for a given resin backbone is a common source of incomplete cure. Aliphatic isocyanate-based hardeners are generally chosen for coatings that need UV stability, such as exterior paint finishes, while aromatic types cure faster but yellow under sunlight. Aliphatic polyester-compatible grades are common in wood-based panel coatings, where moisture resistance and fast recoat times matter more than UV performance. There are also low-VOC and waterborne-compatible hardener variants developed for facilities under stricter emission targets. Each type carries its own working pot life, typically ranging from 30 minutes to several hours depending on ambient temperature and catalyst loading, and mixing the wrong hardener family with a resin never designed for it is one of the fastest ways to get a soft, under-cured surface no matter how carefully the ratio is measured.
Features That Determine Cure Quality
A well-formulated hardener should give a predictable pot life, a defined tack-free time, and a final hardness that matches the resin's design spec — usually verified with a pencil hardness or Shore D test after full cure, which for many two-component systems takes 5 to 7 days at room temperature. Reactivity is temperature-sensitive: a hardener that cures properly at 25°C can under-perform badly at 15°C, which is why cure schedules always list a minimum substrate temperature. Viscosity also matters more than most applicators expect. A hardener that is too viscous for the resin blend resists even dispersion, leaving pockets of resin-rich or hardener-rich film that cure unevenly. These features are why chemical additives should be selected as a matched system with the base resin, not swapped independently based on price alone.
Hydroxyl Resin Hardener Application Areas
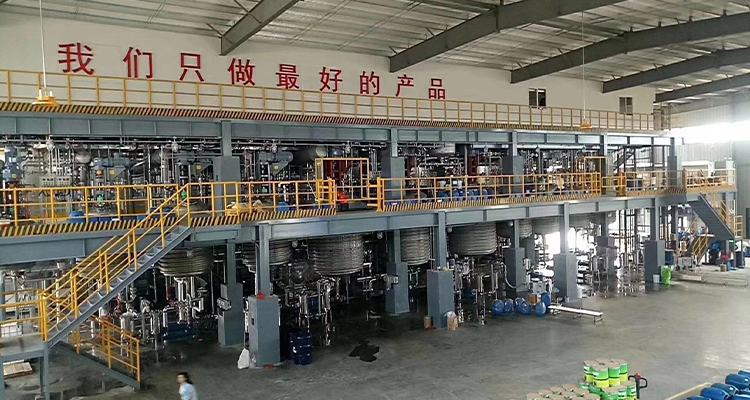
This class of hardener shows up across several industrial coating and molding processes. In PU sole and PU car carpet manufacturing, it works alongside shoe sole paint systems to lock in surface color and abrasion resistance without leaving a tacky finish that picks up dust on the line. In wood-based panel production, it crosslinks surface coatings so panels can be stacked and shipped without blocking. Paper coatings for food-contact applications rely on fast, low-migration cure chemistry, and metal die casting operations use compatible hardeners in mold-release and surface-treatment steps alongside a proper release agent. Color-critical work, such as tinted PU components, often pairs the hardener with a pu paste & pigment system, since pigment load and dispersion quality can shift the cure profile if not accounted for in the ratio.
Hydroxyl Resin Hardener Price Factors
Pricing on curing agents varies more than buyers expect, and quoting purely by kilogram without checking these variables leads to mismatched budgets later.
| Cost Factor | Impact on Price | Notes |
|---|---|---|
| Chemical backbone (aliphatic vs aromatic) | Aliphatic typically 15-30% higher | Aliphatic chosen for UV-stable finishes |
| Order volume | Lower per-kg cost at higher volume | Sholee accepts orders with no MOQ, so small trial batches don't carry a volume penalty |
| Customization | Custom reactivity or viscosity adds cost | Useful when matching an existing resin line |
| Packaging and freight | Drum size and shipping distance affect landed cost | Confirm incoterms before comparing quotes |
A common mistake is comparing two supplier quotes without matching the solids content or reactive equivalent weight — a cheaper hardener on paper can require more grams per batch, erasing the apparent savings once actual consumption is calculated.
Diagnosing Soft or Tacky Cured Films
When a film stays soft after the expected cure time, the diagnosis should follow a fixed order rather than guessing at random. Checking causes out of sequence wastes trial batches and hides the real problem behind a secondary one.
- Check the resin-to-hardener ratio first. An under-dosed hardener leaves unreacted -OH groups, giving a permanently soft, rubbery film that never fully hardens even after extended time. Over-dosing, by contrast, often shows as a brittle or hazy surface rather than softness — so if the film is soft and slightly sticky, suspect under-dosing before anything else. Re-weigh both components on a calibrated scale; volumetric mixing cups are a frequent source of ratio drift.
- Check for moisture contamination second. Isocyanate-based hardeners react with ambient or substrate moisture before they can react with the resin, consuming reactive groups and leaving CO2 bubbling or a soft, uneven film. This shows up more in humid seasons or on substrates stored in damp warehouses. If the ratio checks out but the film is soft with tiny surface bubbles, moisture is the likely culprit.
- Check mixing quality third. Even with a correct ratio, poor mixing leaves micro-zones of unreacted resin. Symptoms include patchy tack — some spots cure hard, others stay soft on the same panel. Hand mixing without a mechanical stirrer, or mixing for less than the specified time (often 2-3 minutes minimum for viscous systems), is the usual cause.
- Check cure energy last. If ratio, moisture, and mixing all test correctly but the film is still uniformly soft, the substrate likely didn't receive enough heat or dwell time to complete the crosslinking reaction. This is common when line speed increases without adjusting oven temperature, or when ambient cure is attempted below the hardener's minimum working temperature.
| Symptom Pattern | Most Likely Cause | Quick Check |
|---|---|---|
| Uniformly soft, rubbery, no bubbles | Hardener under-dosed | Re-weigh both components |
| Soft with fine surface bubbles | Moisture contamination | Check substrate and ambient humidity |
| Patchy — some areas hard, some soft | Poor mixing | Confirm mixer type and mix time |
| Uniformly soft, no bubbles, ratio confirmed | Insufficient cure energy | Verify oven temperature and dwell time |
Buyer's Checklist Before Ordering
- Confirm the hardener's chemical family matches your existing resin backbone.
- Request the recommended mix ratio and pot life at your actual plant temperature.
- Ask whether the supplier accepts small trial orders — Sholee works with no minimum order quantity, which helps when validating a new resin-hardener pairing before scaling up.
- Check typical lead time against your production schedule; Sholee's standard lead time runs around 30 days.
- Verify whether the hardener needs a specific release agent or pigment paste compatibility check before full production.
Sourcing a Hydroxyl Resin Hardener Supplier
Sholee Chemicals supplies release agents, chemical additives, color paste, and paint curing agent products, including customized industrial release agent and hardener formulations built around a customer's existing resin line. Our work covers PU soles, PU car carpets, wood-based panels, food-contact paper coatings, and metal die casting, so formulation adjustments account for how the hardener interacts with pigments, release agents, and cure conditions already in use on the customer's line. Orders ship with no MOQ requirement and a standard 30-day lead time, which makes small validation batches practical before committing to full production volume. The aim is straightforward: give customers a hardener that matches their process instead of forcing the process to adjust around the chemical.
FAQ of Hydroxyl Resin Hardener
How long should I wait before testing final hardness?
Most two-component systems need 5 to 7 days at room temperature to reach full cure. Testing hardness earlier can wrongly suggest a hardener defect when the film simply hasn't finished crosslinking yet.
Can I fix a batch that already cured soft?
If the ratio was under-dosed and the film hasn't fully cured, applying a thin, correctly-dosed topcoat can sometimes rescue it. Once a film has fully reacted with insufficient hardener, though, re-coating rarely restores full hardness — the batch usually needs to be reworked from the mixing stage.
Does color paste affect cure time?
Heavy pigment loading can slow cure slightly by diluting the reactive resin content per volume. If you're using a color paste, confirm the recommended loading percentage with your supplier before adjusting the hardener ratio.
What's the difference between pot life and cure time?
Pot life is how long the mixed hardener and resin stay workable before viscosity rises too much to apply. Cure time is how long the applied film needs to fully crosslink into its final hardness. A short pot life doesn't necessarily mean a fast full cure.
If you're troubleshooting a soft cure batch or need a hardener matched to your existing resin and release agent system, contact Sholee Chemicals to request a quote or a technical sample for trial testing.